

Introduction
This roll-to-roll transfer coating line is designed for the continuous processing of nitrocellulose (NC)-based functional membrane materials and other compatible membrane formulations.
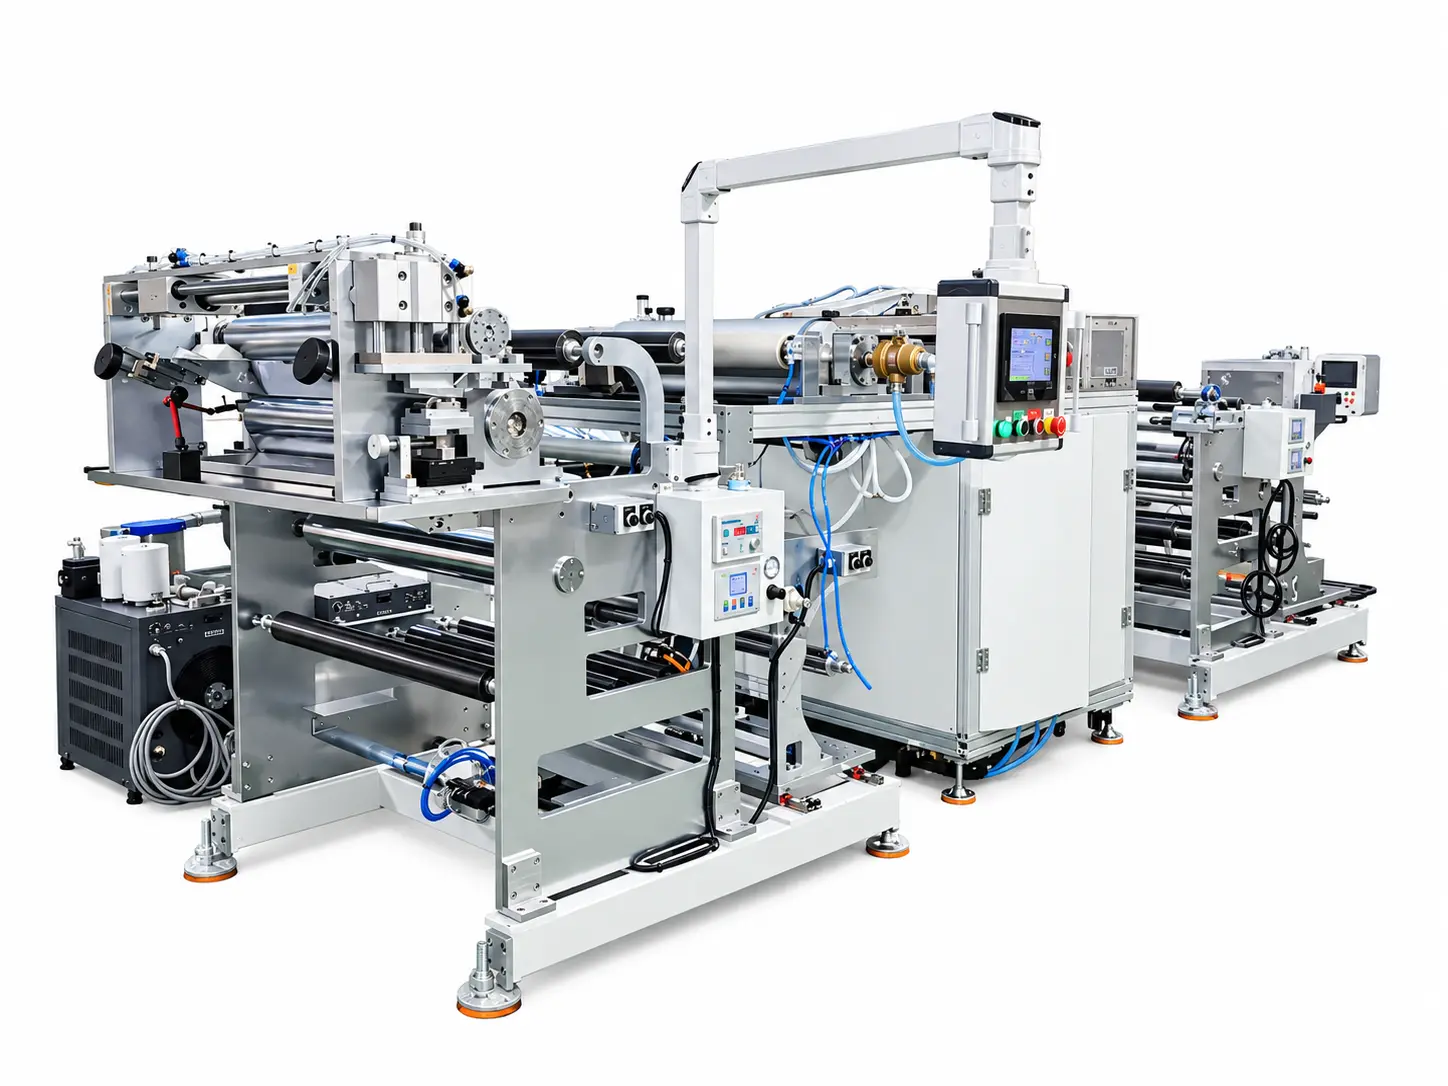
The system transfers coating material from a coating roller onto a moving substrate. It supports both continuous and intermittent coating, with the intermittent mode achieved through controlled movement of the rubber roller assembly.
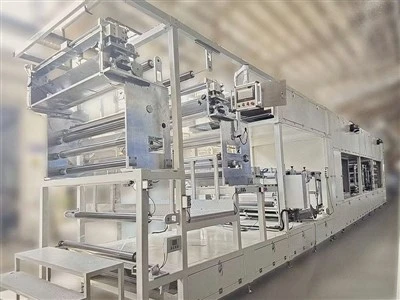
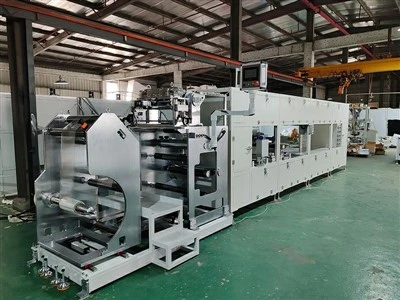
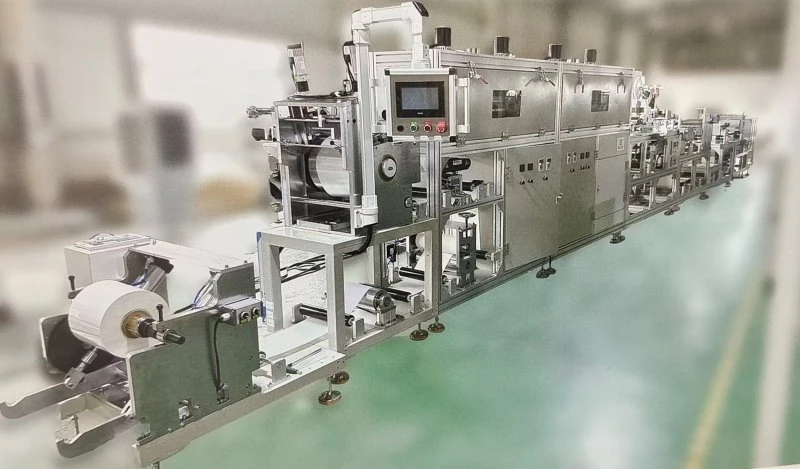
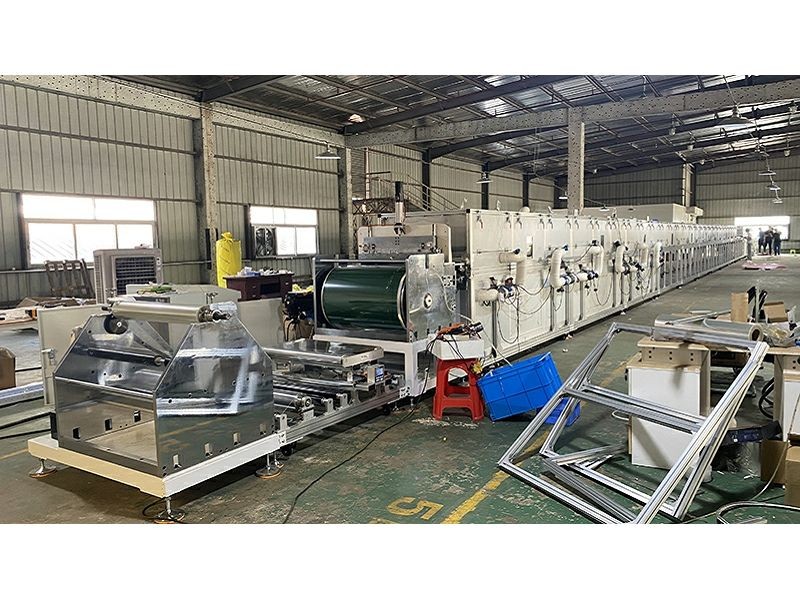
The integrated production line combines web unwinding, tension control, roll transfer coating, temperature and humidity conditioning, primary drying, washing, secondary drying, web guiding, and rewinding.
Designed for process-specific configuration, the line allows key coating and post-treatment parameters to be adjusted according to the formulation, substrate, and required membrane properties.
Parameter
|
Parameter |
Specification |
||
|
Power Supply |
Single-phase AC 220V ±10% / Three-phase AC 380V ±10%, Frequency 50Hz |
||
|
Total Power |
74 kW |
||
|
Compressed Air Supply |
0.5–0.8 MPa compressed air |
||
|
Coating Type |
|
||
|
Applicable Slurry Systems |
Capacitor slurries, pharmaceutical slurries, polymer composites, etc. |
||
|
Guide Roll Width |
Standard: 750 mm (customizable) |
||
|
Substrate Width |
Max. 650 mm (customizable) |
||
|
Coating Width |
600 mm, adjustable via baffles (customizable) |
||
|
Mechanical Speed |
1.5 m/min |
||
|
Coating Speed |
Max. 0.5–1.5 m/min |
||
|
Coating Thickness |
Single-side wet thickness: 0.6–1 mm (determined by slurry; refer to material requirements) |
||
|
Thickness Accuracy |
≤ ±10 μm (excluding abnormal edge areas) |
||
|
Doctor Blade Adjustment |
Manual / automatic adjustment, 1 μm display accuracy |
||
|
Coating Areal Density Variation |
≤ ±1.5% (including substrate; excluding abnormal edge areas) |
||
|
Coating Length |
Roll-to-roll, margin 5–8 mm, accuracy ±0.5 mm (customizable per substrate) |
||
|
Double-side Alignment Accuracy |
±0.5 mm (in length direction) |
||
|
Slurry Hopper Volume |
Approx. 5 L (customizable) |
||
|
Backing Roll Diameter |
Φ800 mm, runout ≤ 3 μm (customizable) |
||
|
Rubber Roll Diameter |
Φ150 mm (customizable) |
||
|
Doctor Blade Diameter |
Φ80 mm (customizable) |
||
|
Drying Oven |
Hot air circulation, total length 18 m |
||
|
Drying Temperature |
Max. 50–60 °C |
||
|
Tension Control |
5–40 N |
||
|
Max. Unwind/Rewind Roll Diameter |
Max. Φ600 mm (customizable) |
||
|
Unwind/Rewind Core ID |
Max. Φ76 mm |
||
|
Operating Side |
Right side (along web travel direction) |
||
|
Machine Dimensions |
L 6200 mm × W 1200 mm × H 1650 mm (customizable) |
||
|
Weight |
Approx. 5000 kg (customizable) |
Key Features
Roll-to-Roll Transfer Coating: Transfers coating material from the coating roller to the substrate in a continuous web-processing setup.
Continuous and Intermittent Coating: Accommodates different coating patterns through controlled movement of the rubber roller assembly.
Adjustable Coating Conditions: Roller settings and relative roller speeds can be optimized to regulate coating transfer and coating weight.
Integrated Temperature and Humidity Conditioning: A 30 m conditioning chamber provides space for process-specific environmental control.
Multi-Stage Drying and Washing: Combines a 6 m primary drying oven, a 2 m washing tank, and a 12 m secondary drying oven.
Integrated Web Handling: Tension control, traction, and four web guiding systems help maintain stable material transport through the line.
Application-Specific Configuration: Roller dimensions, working width, environmental conditions, and selected process parameters can be customized to suit the material and production requirements.
Main Machine Configuration
The production line consists of the following major assemblies:
Unwinding system
Two tension control units
Two traction units
Roll transfer coating unit
30 m temperature and humidity conditioning chamber with conveyor belt
6 m primary drying oven, divided into three 2 m sections
2 m washing tank
12 m secondary drying oven, divided into six 2 m sections
Four web guiding systems
Rewinding system
The final equipment layout and the arrangement of the process sections will be determined during engineering design.
Product Details
5.1 Roll Transfer Coating System
The roll transfer coating system transfers coating material from the coating roller onto the moving substrate through the interaction between the coating roller and the backing roller.
Coating performance can be optimized by adjusting the roller settings and relative roller speeds according to the formulation, substrate properties, and target coating requirements.
The system supports two coating modes:
Continuous Coating: For applications requiring a continuous coating layer.
Intermittent Coating: The movable rubber roller assembly enables coating transfer to start and stop, creating designated coated and uncoated sections.
Coating thickness, coating weight, and pattern accuracy depend on the material properties, machine settings, and operating conditions.
5.2 Temperature and Humidity Conditioning Chamber
The production line is equipped with a 30 m temperature and humidity conditioning chamber with an integrated conveyor belt.
The chamber provides a controlled environment for processing coated materials before the subsequent drying stage. Temperature, relative humidity, and residence time can be configured according to the requirements of the coating formulation and membrane formation process.
This section is designed to support process-specific environmental conditioning and help maintain consistent processing conditions.
5.3 Primary Drying Oven
The 6 m primary drying oven consists of three 2 m sections.
The segmented design provides flexibility for configuring the initial drying profile according to the coating formulation, substrate, and required processing conditions. Independent temperature control can be configured for each section as required.
5.4 Washing Tank
The integrated 2 m washing tank provides an intermediate washing or liquid-treatment stage within the production line.
Depending on the material and process requirements, this section can be configured for washing compatible residues or exchanging process liquids. The washing medium and operating conditions are selected according to the formulation and material compatibility.
5.5 Secondary Drying Oven
The 12 m secondary drying oven consists of six 2 m sections and is positioned after the washing stage.
It provides additional drying capacity to remove residual moisture or other volatile components before the material enters the rewinding section. The drying profile can be tailored to the material characteristics and required final condition.
5.6 Web Tension and Traction System
Two tension control units and two traction units coordinate web movement through the production line.
The tension control units help maintain appropriate web tension during coating and post-treatment, while the traction units provide the driving force for material transport through the different process sections.
Proper tension and traction settings help reduce web slack, excessive stretching, and transport instability.
5.7 Web Guiding System
Four web guiding systems are integrated into the production line to correct lateral web deviation at different processing stages.
They help maintain substrate alignment during coating, conditioning, washing, drying, and rewinding, supporting stable web handling along the extended production path.
5.8 Unwinding and Rewinding Systems
The unwinding system provides continuous substrate feeding into the production line, while the rewinding system collects the processed membrane material into rolls.
Both systems are designed to work with the tension control, traction, and web guiding units to support coordinated roll-to-roll operation. Unwinding and rewinding specifications can be customized according to the substrate dimensions and roll requirements.
5.9 Coating Thickness Adjustment
Coating thickness is influenced by the coating roller settings, relative roller speeds, formulation viscosity, substrate properties, and web speed.
The machine supports manual or automatic adjustment, depending on the selected configuration, with a stated adjustment display resolution of 1 μm.
Note: The 1 μm display resolution refers to the adjustment display and does not represent a guaranteed coating thickness accuracy. Actual coating thickness and uniformity depend on the material and process conditions.
Applications
The line is intended for the roll-to-roll coating and processing of nitrocellulose-based functional membrane materials.
Potential applications include:
Nitrocellulose-based functional membranes
Specialized membrane materials compatible with the selected coating and post-treatment proces
Porous and functional membrane development
Customized membrane coating processes requiring continuous or intermittent coating
Suitability for a particular application must be assessed based on formulation chemistry, solvent compatibility, coating rheology, substrate properties, membrane formation requirements, and downstream treatment conditions.
Applications such as diagnostic membranes or other regulated products should be confirmed separately through material trials and the relevant equipment and process qualification requirements.
Products Detial Images


Hot Tags: Nitrocellulose (NC) Membrane Coating Production Line - Innate, China Nitrocellulose (NC) Membrane Coating Production Line - Innate manufacturers, factory, Automated needle pressing coater, Automated Needle Pressing Equipment, automation equipment, Coating Line for Chemical test paper, NC Nitrocellulose Membrane Coating Line, NC Nitrocellulose Membrane Coating Production Line