The rubber in a thermal pad carries alumina. The adhesive in a flame-retardant tape carries aluminium hydroxide. A ceramic release layer is mostly powder by volume. These formulations share one feature. Most of the solid is inorganic filler, not resin.
The viscometer reading is modest, and the transfer head in a catalogue covers it. The case for transfer metering writes itself. Good precision on thin films, and line speed to spare.
On the line the trouble starts on day three. Shallow patches show up on the web, in no fixed place. Weigh the coat and it runs lighter than on start-up day. Two weeks later the patches have joined up, and no speed setting brings the weight back.
The filler has not changed and neither has the viscosity. What changed sits on the roll surface. Can a filled slurry actually run on a gravure roll?
How Much Room the Opening Leaves for Particles
A gravure roll feeds the web from small cells engraved into its surface.
On a 250-line roll the cell opening runs around eighty microns. On a 400-line micro-gravure it is twenty to thirty. The formulation sheet lists a D50 of two or three microns for the filler, which looks comfortably below the opening.
A particle size distribution is not a line. D50 is the median, and half the particles are larger. A D99 above twenty microns is common in inorganic fillers, and agglomerates double it. A few large ones bridge the opening, the cell cannot fill, and the web comes out light in that spot.
A blocked cell does not clear itself. Slurry sits in the cell, solvent leaves, and the skin takes up more of the volume. The extra patches on day three mostly start there. How coarse the filler runs is the first question a coating machine manufacturer should ask at the selection stage.
When an equipment supplier sends the sample request, ask for the particle size distribution with it. Where the figures stop at D50, ask them for a D99. That column decides how many oversize particles you will meet.
What Filler Hardness Wears Away
Wear is the second account.
Alumina sits at 9 on the Mohs scale, quartz at 7, aluminium hydroxide and calcium carbonate around 3. Once the filler out-hardens the blade and the roll face, wear runs on a daily basis.
On gap metering the wear lands on the blade edge. The gap opens slowly, and the direction and the rate are easy to read. On a gravure roll the wear lands on the cell walls and the cell floor. The cells shallow out and widen, the volume grows, and the roll carries more slurry month after month. You can spend weeks going through the formulation while the problem sits in the roll volume.
A ceramic face resists this far better. A chromium oxide coated roll with a carbide blade does wear, only slowly. The price sits in cost and lead time, and a regrind has to be scheduled. Ask a supplier for the regrind allowance figure. One who cannot answer has probably never run a hard filler. Where the supply of a ceramic roll and its regrind intervals stand, a coating line manufacturer should state at the quotation stage.
Two Drifts on One Roll
On paper these are two problems. On the roll they wear one face.
Blocked cells pull the transfer ratio down. Worn cells push it up. Running against each other, they cancel for a while and the coat weight looks steady. When blocking wins, the figures fall. By then, can you still tell which drift to blame on which day?
Weigh-Ins and a Trial Separate the Two
Start with weigh-ins. Weigh once on start-up day, then weekly at the same position. The theoretical coat weight comes from the cell volume. How far the measured value drifts around it is the margin this roll has left. A coating line supplier who lays down that baseline during installation hands you the reference for every week after.
A trial does the same job. Have a machine builder run your slurry on a roll in their shop for half an hour, and weigh before and after. A fresh roll that already weighs out light points at blocking, not at wear.
Measure Size and Hardness Before You Pick a Roll
Split the question on the D99 and the Mohs hardness of the filler. Most cases answer themselves.
Where D99 sits inside a quarter of the cell opening and the hardness stays below the roll face, a gravure roll runs steady. Add low solids and it runs that way for years. Soft fine filler on a low-line roll goes a long time without trouble. The cleaning interval belongs in the maintenance plan a coating line manufacturer writes.
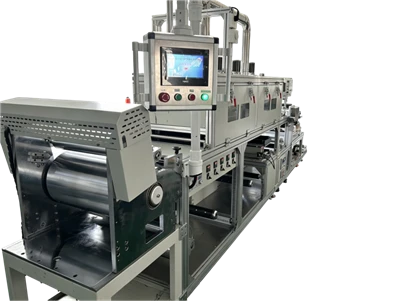
Where D99 approaches the opening and the hardness runs high, change routes. A comma blade works with a gap in the two to three hundred micron range. That is two orders of magnitude above the particles. There are no cells to block. Filler passes out of both sides of the gap, and wear lands on the blade line. Swapping a blade costs less than swapping a roll. A slot die can carry it as well. The anti-settling circulation never stops, and the lip wear is budgeted for hard filler.
Which route fits is a question of experience. A coating machine manufacturer who states the line count in the proposal has run filled systems. The expected cleaning interval and the roll face material belong on the same page. Ask the manufacturer straight out whether they have run your filler, and the way the answer comes back tells you. The roll face treatment sits in the assembly records of a machine builder, ceramic or chrome plated, one page apart. A machine builder who attaches a measured cell volume and a wear reference curve gives every later drift something to be checked against. A proposal from an equipment supplier that lists a viscosity but never mentions the filler can wait. Ask a supplier for these figures, and see whether the answer arrives in writing.
Where an OEM coordinates the project, regrind allowance, cleaning interval and a spare roll belong in one list, checked at handover. The cleaning agent and the ultrasonic settings for your filler are worth walking through with a coating line supplier during commissioning. Where an OEM runs the project, the acceptance day goes down that list item by item.
Whether a filled slurry runs on a gravure roll, check once more when the proposal from a coating machine manufacturer arrives. Size that passes the opening and hardness that does not beat the roll face, and the precision of gravure metering stays yours. Fail either one and gap metering is the simpler route, with precision to spare.
That set of requirements comes down to how particle size, hardness and the metering method are matched. Problems like this come up often in custom work. Innater works precision, thickness and uniformity out against your filler and your target thickness, machine by machine.
Write the D99 and the Mohs hardness of the filler into the technical agreement, beside the viscosity. Without those two figures the line count on the proposal is copied from a catalogue.

material feeding system-Innate

doctor blade coater-Innate
Published by Innater Intelligent Equipment Co., Ltd, a maker of non-standard coating machines and automated lines. Email 13316631159@163.com | Website https://www.getinnater.com/ | Tel +8613316631159